

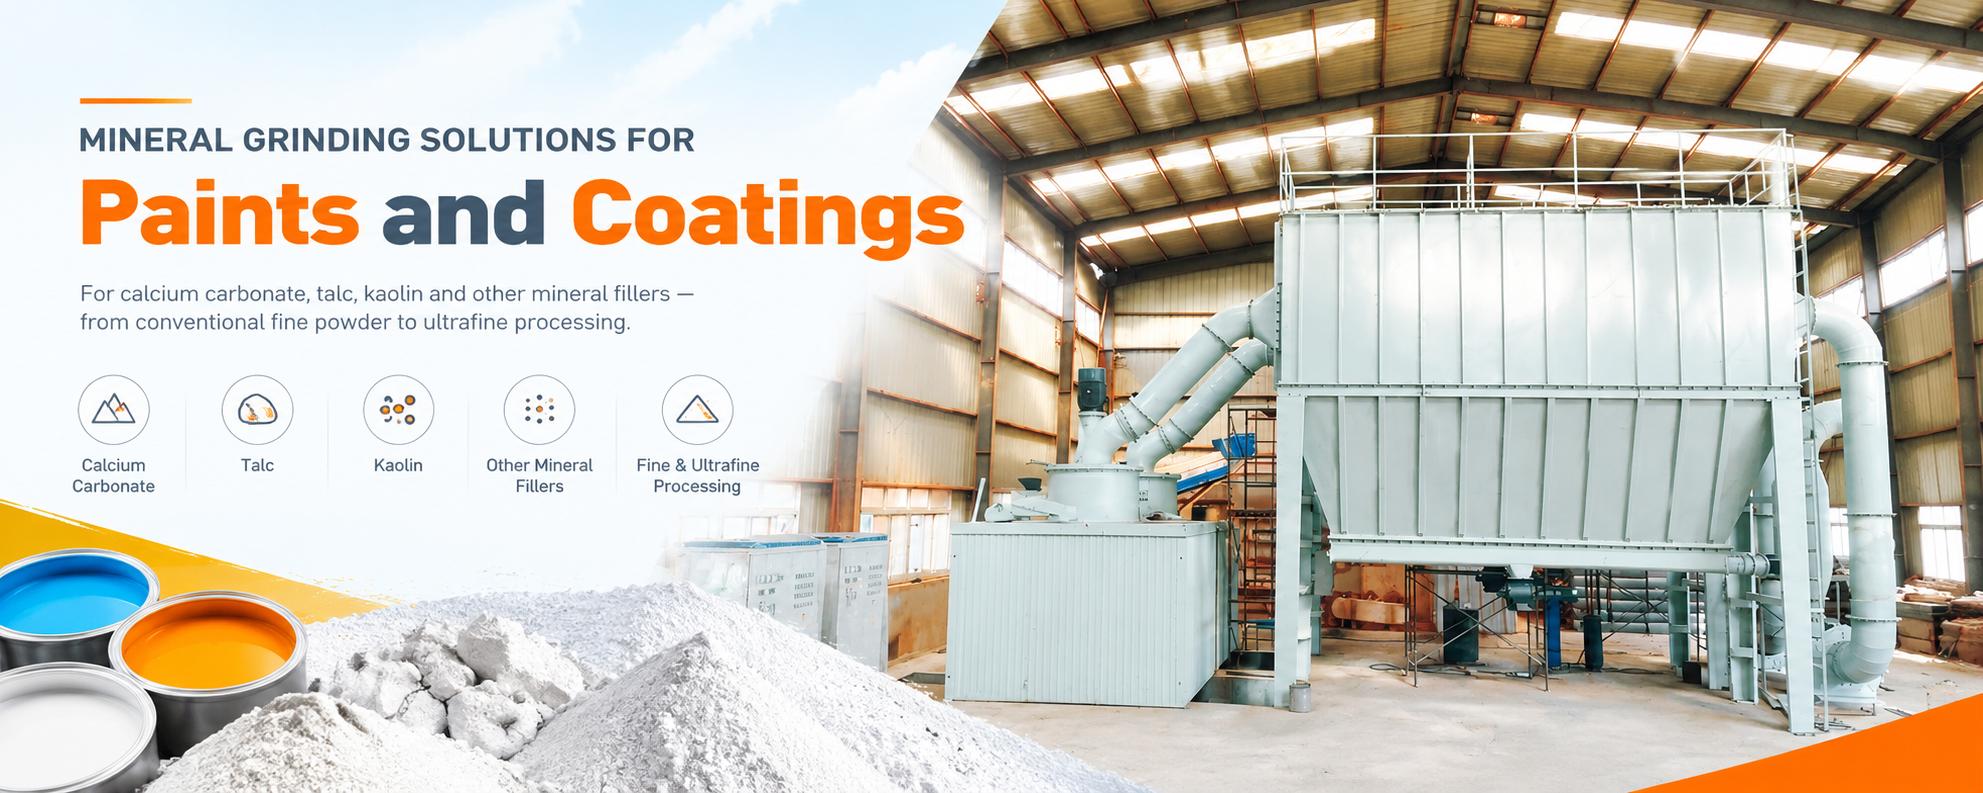
Fine powder classification separates a mineral powder into fractions with different particle-size characteristics. In paint and coating filler production, its main purpose is to control the finished distribution—particularly the coarse particles that can affect surface smoothness, dispersion, and batch consistency.
Grinding and classification perform different jobs. The mill reduces particle size; the classifier determines which material can leave as finished powder and which must be rejected or returned for further grinding. A well-designed line coordinates both functions rather than relying on more intensive grinding to solve every quality problem.
Why a Fine Median Size Can Still Produce a Rough Coating
A calcium carbonate, talc, or kaolin powder may meet its median particle-size requirement while containing an unacceptable coarse fraction. The majority of the powder can be sufficiently fine, yet occasional hard particles or persistent agglomerates may remain visible in a thin coating.
This is where classification becomes especially useful. It helps manage the distribution leaving the grinding circuit instead of allowing all ground material to become finished product.
However, classification is not an absolute barrier against every oversize particle. Separation efficiency, equipment condition, material dispersion, and operating stability all influence the result. Where a customer requires strict coarse-residue control, verify it with a separate acceptance test rather than assuming that the classifier setting guarantees compliance.
What Happens Inside a Dynamic Air Classifier?
A dynamic air classifier uses controlled airflow and a rotating classifier wheel to separate particles according to their aerodynamic behavior. Fine particles are carried through with the air, while particles that are more strongly rejected by the rotating system report to the coarse fraction. Size, density, and shape all influence this separation.
In a closed grinding circuit, rejected material returns to the mill for further size reduction. In a separate classification operation, the coarse fraction may be collected as another product or sent for reprocessing.
Unlike a sieve, an air classifier does not separate material through fixed mesh openings. This makes it useful for fine mineral powders, but it also means that the result cannot be understood as a simple physical screen limit.
The cut point is not the largest particle in the product
A classifier's cut point describes its separation behavior. It is commonly associated with the particle size having an equal probability of reporting to either outlet, under the stated definition and test conditions.
That is different from the D50 of the finished powder, which describes the median of the product distribution. It is also different from the product's D97 or its largest observed particle. Keeping these terms separate prevents misunderstandings when discussing equipment performance.
Choose the Classification Duty Before Choosing the Settings
Different coating fillers require different separation objectives. A classifier should be configured around the actual product problem rather than simply adjusted toward the finest possible powder.
| Production objective | What classification must achieve | What to verify |
|---|---|---|
| Reduce coarse particles in a smooth-coating filler | Limit the coarse tail without unnecessarily reducing the whole product distribution | Coarse residue, high-percentile particle sizes, and coating appearance |
| Produce an ultrafine calcium carbonate grade | Coordinate fine-particle recovery with sufficient rejection of coarser material | Full distribution, stable output, and energy consumption |
| Process talc or kaolin for morphology-sensitive applications | Separate the required fraction while accounting for plate-like particle behavior | Distribution, particle morphology, and formulation performance |
| Manufacture several grades from one feed | Deliver repeatable distributions at different operating points | Output by grade, adjustment time, and transition-material handling |
A single classification stage should not automatically be expected to produce a narrowly bounded size fraction. If the specification requires removal of both coarse particles and excessive ultrafines, the process may need additional separation stages or a different circuit arrangement.
Four Variables That Must Be Adjusted Together
Classifier speed
In a typical dynamic centrifugal classifier, increasing wheel speed generally produces a finer separation, provided other conditions remain comparable. More material may be rejected for further grinding, so finished-product output can decrease as the specification becomes finer.
Airflow
Airflow carries particles through the system and influences their passage through the classifier. Increasing airflow can allow larger particles to enter the fine stream, while insufficient airflow may impair transport. Rotor speed and airflow therefore need coordinated adjustment rather than independent optimization.
Feed rate and loading
The classifier must receive a stable, appropriately dispersed material stream. Excessive loading can interfere with effective separation, while fluctuating feed makes it difficult to maintain a consistent distribution.
When the finished powder becomes coarser, increasing classifier speed may not address the underlying issue if the system is overloaded or the feed is poorly dispersed.
Feed condition
Moisture, agglomeration, and changes in mineral composition can alter classification behavior. A soft cluster of fine particles may behave differently from individually dispersed particles, and minerals of different density or shape may separate differently at the same settings.
Record feed condition alongside operating parameters. A successful setting for one raw-material batch should not be assumed to transfer unchanged to every subsequent delivery.
Classification Cannot Replace Mineral Purification
Air classification can reject some unwanted material when it differs sufficiently in aerodynamic behavior from the desired powder. It is not, however, a dependable substitute for removing all iron-bearing impurities, quartz, or other contaminants.
Some contaminants may be similar in size and aerodynamic behavior to the useful mineral and pass into the finished product. Others may become fine enough to pass after repeated grinding.
If purity, whiteness, or abrasive impurities are critical, establish suitable raw-material controls and any necessary beneficiation before final classification. Do not assume that a finer classifier setting will produce a purer mineral.
Integrating Classification with Liming Heavy Industry Grinding Mills
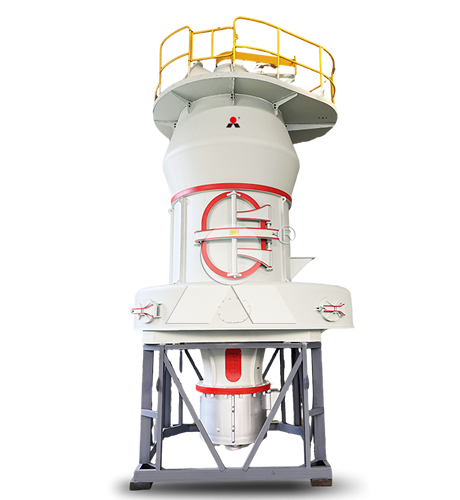
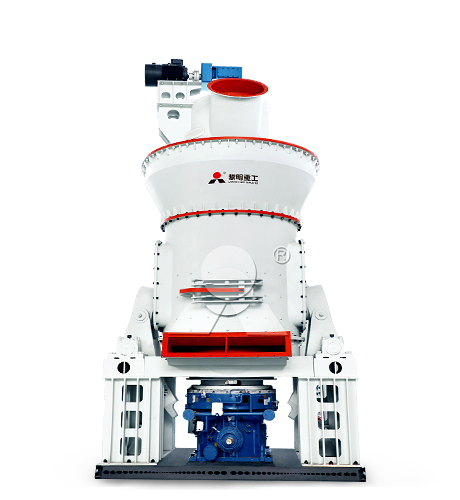
For ultrafine mineral-filler projects, the Liming Heavy Industry LUM Ultrafine Vertical Mill provides an integrated grinding and classification arrangement. Its variable-frequency multi-rotor classifier is used to adjust product fineness, with feed characteristics, airflow, and operating conditions also influencing the result.
When evaluating a LUM system, define the required finished distribution and coarse-residue limit before finalizing the configuration. Ask for the proposed output at that specification, not simply the broad fineness range available from the equipment family.
The evaluation should also establish how rejected material returns to the grinding zone and how increasing internal circulation affects capacity and operating stability. A finer product may require more recirculation, additional grinding, or a lower feed rate.
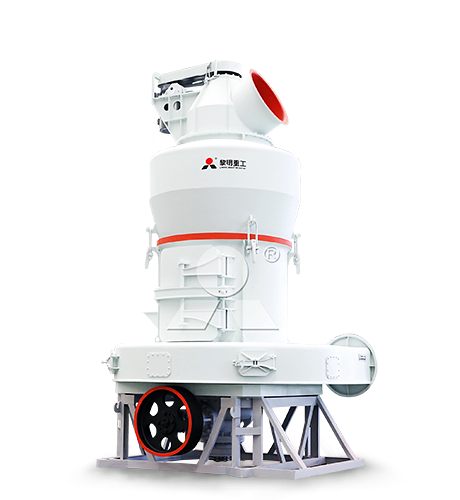
For other Liming Heavy Industry grinding configurations, apply the same principle: assess the mill, classifier, airflow system, and collection equipment as one process. A capable classifier cannot compensate indefinitely for unsuitable grinding conditions or an unstable feed.
When the Product Changes: A Troubleshooting Sequence
If a previously acceptable powder becomes inconsistent, avoid changing several settings at once. First confirm the laboratory result, then investigate the process systematically.
| Symptom | Possible cause | Practical check |
|---|---|---|
| The coarse end increases suddenly | Changed airflow, unstable feed, equipment wear, or an unintended bypass path | Review operating trends and inspect relevant components under safe shutdown procedures |
| Output falls after a finer setting is selected | More material is being rejected and recirculated | Check the distribution, circuit loading, and sustained saleable output together |
| Particle-size results fluctuate between samples | Feed variation, moisture changes, unstable operation, or inconsistent sample preparation | Compare timed process samples using one standardized laboratory method |
| The distribution passes but visible specks remain | Isolated oversize particles, contamination, or agglomerates not adequately represented in the test | Examine residue and dispersed coating samples; inspect downstream handling |
| The powder is finer but paint viscosity rises unexpectedly | A larger fine fraction or changed dispersion demand | Compare the complete distribution and repeat the formulation under controlled mixing conditions |
Prove Separation Performance with Representative Samples
The most useful classifier trial measures more than the finished powder. Where practical, sample the incoming material, fine product, and coarse fraction under stable operating conditions. This helps show whether acceptable particles are being unnecessarily rejected or coarse material is entering the fine stream.
A practical acceptance procedure should include:
An agreed sampling method and consistent particle-size measurement procedure.
The full distribution curve, not only one median value.
A coarse-residue test appropriate to the coating application.
Timed samples demonstrating stability during continuous operation.
Measured saleable output and clearly defined energy-consumption boundaries.
Color, moisture, or morphology checks where these are critical.
Coating trials confirming dispersion, appearance, and application behavior.
Use consistent sample dispersion conditions. A classification trial can be misjudged if one laboratory fully disperses soft agglomerates while another measures them as coarse particles.
Protect the Separation Result After Collection
Once acceptable powder leaves the classifier, clean handling remains essential. Residual material in shared conveyors, dirty silos, or contamination at the filling station can reintroduce coarse particles that the classification system has already controlled.
Include grade segregation, cleaning access, batch identification, and downstream sampling points in the line design. For frequent product changes, define how transition material will be collected and evaluated before the next grade is released.
For a new line or an upgrade, provide Liming Heavy Industry with representative feed, an approved reference powder, the required distribution, coarse-residue limits, and output by grade. The objective is repeatability: a classification system that consistently delivers the filler required by the coating formulation, rather than merely producing a favorable laboratory sample.
Related Mineral Grinding for Paints & Coatings


LIMING at MiningMetals Uzbekistan 2026 | Booth B94
2026-10-22

LIMING Heavy Industry at MINEXPO Africa 2026 | Booth 133
2026-10-22
Liming Heavy Industry to Exhibit at bauma CHINA 2026 – Visit Us at Booth E6.510
2026-10-15
Meet Liming Heavy Industry at the 140th Canton Fair 2026
2026-10-13
Liming Heavy Industry to Attend the 140th Canton Fair
2026-09-25
Complete Mineral Processing Solutions
Convenient Reliable Professional Efficient Get Your Quote
Please feel free to submit your inquiry information to us. We will contact with you as soon as possible.
Our team will contact you as soon as possible.